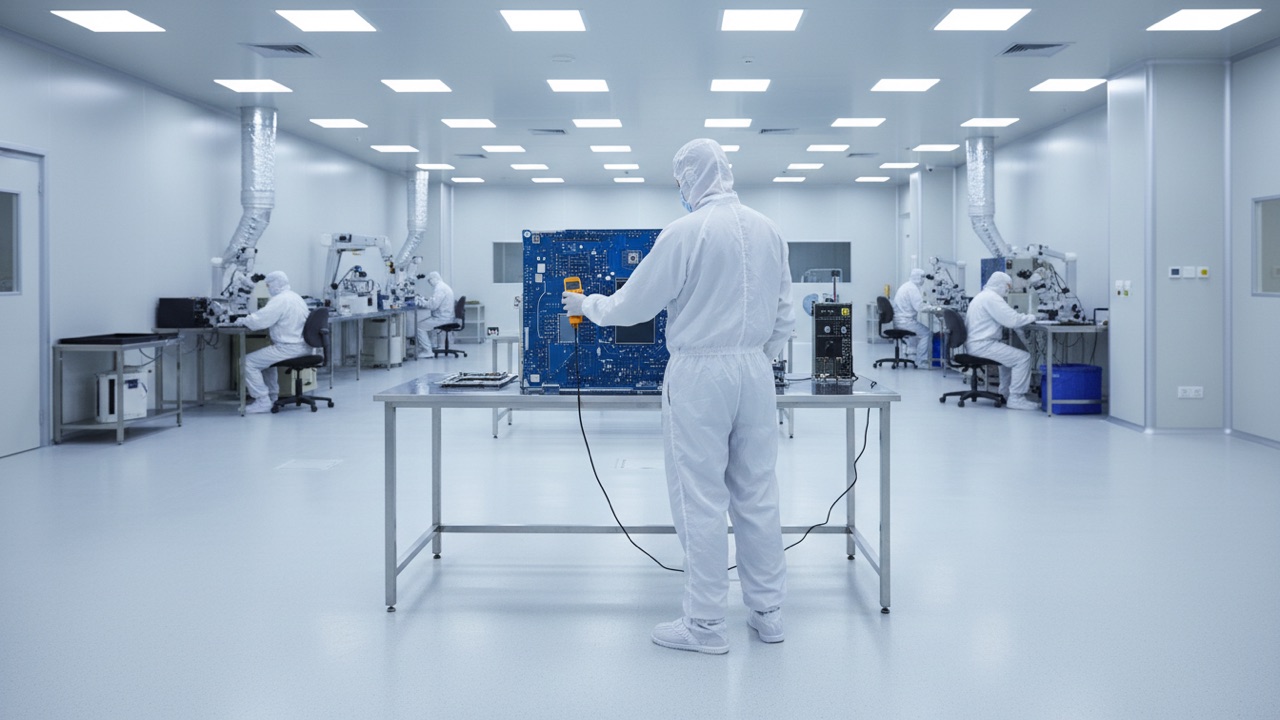
ANSI/ESD S20.20 compliant flooring is a seamless floor system whose electrical resistance to ground falls inside defined limits, is verified by a standard test method and is tied to a working ground path. Specifiers writing for an electronics plant, lab or cleanroom need the numbers, the test method and the documentation to require, and that is what this guide sets out. For the service itself, see our ESD anti-static epoxy page, and for how static control works in a warehouse, see our guide to warehouse ESD static control.
1. Conductive, Dissipative and Antistatic: The Three Categories Defined
Conductive, dissipative and antistatic describe how quickly a floor moves electrical charge, and the category you choose decides what the floor protects. Conductive floors move charge fastest, dissipative floors move it at a controlled rate and antistatic floors only limit how much charge builds up in the first place.
| Category | Resistance range | How it behaves | Typical use |
|---|---|---|---|
| Conductive | Below 1 x 10⁶ ohms | Moves charge to ground quickly | Explosive atmospheres, some electronics assembly |
| Static dissipative | 1 x 10⁶ to 1 x 10⁹ ohms | Bleeds charge at a controlled rate | Most electronics manufacturing |
| Antistatic | Above 1 x 10⁹ ohms | Limits charge generation only | General areas, low sensitivity |
The ranges above are the commonly used ones, and the exact limits come from the standard and the application. A conductive floor is not automatically better. Moving charge too fast can create a rapid discharge that damages sensitive components, which is why dissipative flooring is the default for electronics and conductive flooring is reserved for cases where ignition is the hazard.
2. ANSI/ESD S20.20 Resistance Ranges and What to Specify
ANSI/ESD S20.20 is a program standard for protecting electrostatic discharge sensitive items, and it sets limits on resistance to ground for flooring and for the personnel grounding system that includes footwear. In practice the flooring limit is expressed as a maximum resistance to ground, commonly below 1 x 10⁹ ohms, and the floor and footwear are evaluated together.
IEC 61340-5-1 is the international equivalent and uses a similar limit for flooring. A specification for a project that must satisfy either should state the standard by number, the resistance range required, the test method and the conditions of testing. Leaving any of those out invites a floor that passes one test and fails another.
- State the category: Conductive or static dissipative, not just "ESD".
- State the range: The resistance to ground limits in ohms, with the standard that sets them.
- State the system: Whether the limit applies to the floor alone or to the floor and footwear together.
- State the humidity: Resistance changes with relative humidity, so the test conditions belong in the spec.
Phoenix is dry, and low relative humidity raises static generation, so indoor humidity control is part of the overall static control program, not something the floor can solve on its own.
3. ASTM F150 and How Floor Resistance Is Actually Measured
ASTM F150 measures the electrical resistance of conductive and static dissipative flooring by placing weighted electrodes on the surface and applying a set voltage. It reports resistance between two points on the floor and from the floor to a ground reference.
S20.20 itself points to ANSI/ESD STM7.1 for measuring the resistance of floor materials, and specifications often cite both methods. What matters for a specifier is to name the method, require a calibrated meter, define the number and location of test points and record the humidity and temperature at the time of test. A reading without those conditions cannot be compared with the next one.
| Item to specify | Why it matters |
|---|---|
| Test method (ASTM F150 or ANSI/ESD STM7.1) | Different methods give different readings |
| Number and spacing of test points | Coverage shows uniformity, not one lucky spot |
| Meter calibration and applied voltage | Resistance depends on test voltage |
| Temperature and humidity at test | Readings shift with conditions |
| Pass and fail limits | Removes argument at commissioning |
Cleaning chemistry and wear both change a floor's resistance over time, so periodic retesting is part of the program rather than a one-time event.
4. Grounding the Floor: Copper Strips, Ground Points and Verification
An ESD floor does nothing without a path to ground, which is built in as copper grounding strips embedded under or within the system and connected to building ground at defined ground points. Missing or broken grounding is a common audit finding.
- Lay out the grounding grid: Copper strips are laid on the primed slab in a pattern set by the manufacturer. Data sheets commonly call for a ground point roughly every 1,000 square feet, but follow the product's own requirement.
- Connect to building ground: A licensed electrician connects each ground point to the building grounding system.
- Apply the conductive layers: The conductive primer and topcoat go over the copper so the system is electrically continuous.
- Verify continuity: Test from the surface to each ground point and record the readings.
Because the electrical connection is the electrician's work and the coating is the flooring contractor's, the specification should assign responsibility for each step. If nobody owns the ground connection, nobody checks it, and the floor fails its first audit. The same coordination applies in healthcare areas that combine hygiene and static control, as in our guide to hospital and medical facility flooring.
5. Cleanroom Requirements Layered on Top of ESD
A cleanroom floor has to control particles as well as static, which means a seamless, low-particulating, cleanable surface that is also conductive or dissipative. ISO 14644-1 classifies cleanrooms by the number of airborne particles allowed per cubic meter, and the floor has to avoid adding to that count.
| ISO class | Max particles 0.5 micron and larger, per m3 | Floor implications |
|---|---|---|
| ISO 5 | 3,520 | Seamless, coved, very low particulate |
| ISO 6 | 35,200 | Seamless, coved, low particulate |
| ISO 7 | 352,000 | Seamless, cleanable resin |
| ISO 8 | 3,520,000 | Cleanable resin, controlled traffic |
Commonly the answer is a seamless resinous system formulated to be low-particulating, cleanable to cleanroom protocol and conductive at the same time. The specification has to state both requirements explicitly or you get one and not the other. Coving at walls, sealed penetrations and chemical resistance to the cleaning agents in use follow the same logic as other controlled environments, covered for healthcare in our healthcare epoxy flooring Phoenix page.
6. Commissioning, Testing and the Documentation to Require
Commissioning proves that the installed floor meets the specification, and the documentation it produces is what an auditor or customer will ask for. Require it in the contract so it is delivered at handover rather than chased afterward.
- Product data sheets: For every layer, including primer, conductive layer and topcoat.
- Grounding layout: A drawing showing copper strip routing and ground points.
- Electrician sign-off: Confirmation that each ground point is connected to building ground.
- Resistance test report: Method, instrument, test points, conditions and results against the limits.
- Maintenance instructions: Approved cleaning products, since some leave an insulating film.
- Retest schedule: When resistance will be verified again and by whom.
On cost, our published ESD rates are $10 to $14 per square foot for dissipative systems and $14 to $18 per square foot for conductive systems, shown on our ESD page. Slab condition, moisture, grounding layout and cleanroom requirements change the final figure, so we scope each project after a walkthrough. Production plants with mixed hazards may also want our guide to industrial epoxy flooring in Phoenix, and for a simpler residential floor, our epoxy garage floor Phoenix page covers that system.
7. Choosing Conductive or Dissipative for Your Application
The application decides the category, and the usual rule is dissipative for sensitive electronics and conductive where ignition of vapors, powders or propellants is the hazard. Choosing on cost or habit is how a plant ends up with a floor that protects the wrong thing.
| Application | Usual choice | Reason |
|---|---|---|
| Electronics assembly and test | Static dissipative | Controlled discharge protects components |
| Semiconductor and cleanroom | Static dissipative | Combined particle and static control |
| Explosive or flammable atmospheres | Conductive | Fast charge removal prevents ignition |
| Data centers and server rooms | Static dissipative | Protects equipment and cabling |
| Aerospace and defense assembly | Per program requirement | Follow the contract specification |
If you are unsure, ask the equipment manufacturer or your safety consultant which category their sensitive items require. The floor is one piece of a program that also includes wrist straps, footwear, work surfaces and humidity control, and the standard expects them to work as a system.
8. Common Specification Mistakes to Avoid
Most ESD floor failures trace back to the specification rather than the coating, and a handful of mistakes account for most of them. Catching them on paper is far cheaper than finding them at commissioning.
- Writing "ESD floor" without a category: Conductive and dissipative are different products, and a vague spec lets the bidder choose.
- Omitting the test method and conditions: Without a method, number of points and humidity, results cannot be compared or enforced.
- Forgetting the ground connection: Nobody is assigned to connect the copper to building ground, so the floor is not grounded.
- Specifying ESD but not cleanroom needs: The floor passes resistance and fails on particles, coving or chemical resistance.
- Ignoring the cleaning regime: A polish or cleaner that leaves an insulating film raises resistance above the limit.
- Skipping retesting: Resistance drifts with wear and chemistry, and an untested floor is an unknown floor.
A specification that names the standard, the category, the range, the method, the ground connection and the documentation leaves very little to argue about at handover.
9. Frequently Asked Questions
Free ESD Flooring Consultation
Talk through your facility and specification with our team and get a written scope with test requirements.